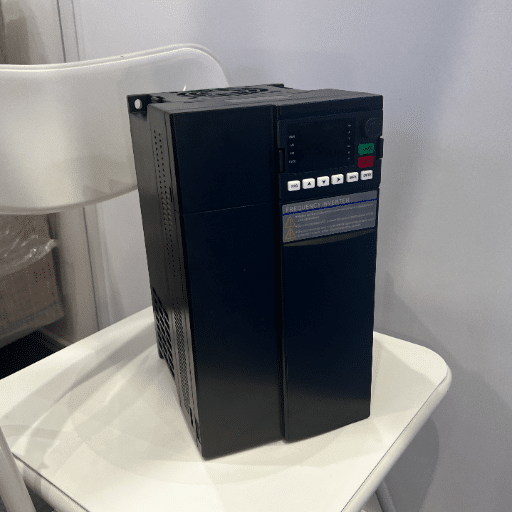
Ready to Get Your VFD Solution?
Whether you need a single drive or a complete system, we have the VFD products and engineering support to ensure your project's success.

A variable frequency drive is built in two halves. First the circuit board is assembled on an SMT line through solder-paste printing, component placement, reflow soldering, and optical inspection. Then the complete machine, assembled, hi-pot tested, functionally tested, aged at high temperature for 24 to 48 hours, inspected, and packed. Every station leaves evidence, and every piece of evidence has limits.
That last part is what most VFD factory pages never tell you. Ask for factory photos and you will receive twelve of them: a spotless SMT line, a wall of certificates, rows of finished drives. All of it looks convincing. None of it proves that the factory in the pictures is the factory that will build your order, and the advice you have probably been given, that a real VFD manufacturer owns its own SMT line, is simply wrong. Most genuine manufacturers outsource board fabrication, and that is normal.
We publish this from inside a VFD factory. Shandong Electric builds drives from 0.1 kW to 53,000 kW, and our engineers walk these stations daily. Below you get the full VFD production line, board to crate: what each station actually proves, what it cannot prove, and the exact question to ask at each one.
Key Takeaways
- A VFD is built in two halves: the board (PCBA) and the complete machine. Genuine manufacturers often outsource board fabrication, so never judge a factory on whether it owns an SMT line
- The complete machine runs a fixed sequence: assembly, hi-pot (withstand-voltage) testing, functional test and debug, 24-48 hour high-temperature aging, final inspection, then packing
- Aging (burn-in) is the one station an assembler cannot afford to fake, because it forces early failures to surface in the factory instead of in your panel
- A factory photo proves a line exists; it does not prove the line will build your order, how parts are torqued, or that the unit was load-tested. Ask for the aging log and the serial-ID range instead
- Run a live video tour against a station-by-station rubric, and keep the certificate file separate from the certificate on the wall

Every drive you will ever evaluate is the product of two separate processes. The VFD manufacturing process runs in two halves, and separating them is the first thing to establish with any supplier.
The first half is the board: the printed circuit board (PCB) populated with components into a finished assembly (PCBA). This is high-precision surface-mount work done on an SMT line. The second half is the complete machine: the assembled unit with its power stage, heat sink, cooling, enclosure, firmware, and testing.
The split matters because the two halves carry different risks. A factory that outsources board fabrication but owns assembly, hi-pot, aging, and load test is a real factory with a real quality system. A factory that owns a shiny SMT line but does no aging is a riskier supplier. Buyers who reverse those two judgments reject good suppliers and shortlist weak ones.
This short primer covers what a drive does before we look at how one is built:

The board half runs on a surface-mount technology (SMT) line, and it follows a sequence you can verify on any tour.
That standard is worth knowing by name: IPC-A-610 sets workmanship and acceptance criteria in three classes. Class 3 is reserved for high-reliability products. It requires 100% joint inspection rather than sampling, X-ray for hidden joints, and full traceability.
Class 3 costs roughly 20% to 40% more than Class 2 and rejects 8% to 15% of assemblies. The IPC-A-610 class system is the language your supplier should be able to speak without prompting. The companion standard, IPC J-STD-001, covers the soldering process itself, so a serious supplier will pair them.
Nadia, a procurement manager for a European panel builder, nearly made an expensive mistake here. She rejected a Chinese factory outright because it did not own its SMT line, and shortlisted a cheaper supplier with a gleaming in-house line. Her engineer pushed back: board fabrication is routinely outsourced industry-wide, and the first factory owned the stations that actually predict reliability.She asked both for aging logs and hi-pot records. The gleaming supplier had neither.The factory she had rejected produced both and won the contract.
After the surface-mount work, a VFD needs parts that SMT cannot place: large capacitors, the IGBT power modules, transformers, inductors, and terminal blocks. This is a through-hole assembly.
Operators insert these parts by hand, which makes skill and process control matter more than on the automated line. The main risks are a wrong position or a reversed polarity, so the step carries a higher inspection load. The board then passes over a wave of molten solder to bond the through-hole joints, typically around 265 to 270 °C depending on whether the process is leaded or lead-free. Optical inspection afterward checks polarity, missing parts, and joint quality against the same IPC-A-610 criteria.
The last board-level step is conformal coating, a protective film that guards electronics against dust, moisture, salt, mechanical vibration, and thermal shock. Coating area and thickness have to be controlled. Applied too thin, it fails to protect, and the product’s service life is not assured. On a tour, ask how coating thickness is verified, because a fast answer here separates a controlled process from a cosmetic one.
The board now becomes a machine. Assembly builds the power stage in order: the rectifier section, the DC bus and filtering, the current-limiting section, the IGBT inverter stage, and the control board, along with the heat sink, cooling fan, and chassis.
Two details at this station predict more than any photo. First, power devices are mounted to the heat sink with controlled torque because heat transfer and long-term reliability depend on it. Second, wiring between the main circuit and the control circuit is routed and dress-checked, because a loose or misrouted connection is a field failure waiting to happen.
Then the unit is tested, and the tests are not decorative.
One honest limit belongs here. Functional test coverage is high, but it is not total, and industry analysis puts it near 98%. A small share of defects can pass a functional test. That is exactly why the next station exists.

Aging, or burn-in, is the reliability centerpiece of a VFD factory. After the unit passes hi-pot and functional test, it runs under power at elevated temperature for a sustained period, commonly 24 to 48 hours and sometimes longer for higher-power or more critical products.
The purpose is to force infant mortality out of the factory. Electronic assemblies tend to fail early or late, not evenly across their life. A weak solder joint, a marginal component, or a thermal problem will often show up in the first day or two of continuous operation.
A factory that runs aging catches those units and repairs or scraps them. A factory that skips it ships them to you, and they fail in your panel weeks later, when the failure costs downtime instead of a rework.
This is the station an assembler cannot afford to fake. An aging room is expensive to run: it consumes floor space, power, and time, and it ties up finished goods. A trading company that rebadges drives, or an assembler with no real test capability, will show you a rack in a photo but not the log behind it.
Published factory tours from other manufacturers describe the same sequence, from hi-pot through aging to final inspection, which tells you this is industry standard rather than one company’s marketing (INHE’s inverter manufacturing base is one public example).
So ask for the log, not the rack. Request the VFD aging test record for your model: serial numbers, hours, and temperature. Ask what happens to a unit that fails aging and who signs off on the disposition.
Chidi, an OEM machine builder sourcing drives for a packaging line, did exactly this. His candidate supplier’s burn-in log showed a batch failing at hour 30 of a 48-hour run. The supplier’s engineer traced it to a component lot and reworked the batch before shipping.
Without that log, Chidi would have received those units and found the fault in his own customers’ machines. “The rack photo meant nothing,” he said. “The log saved the order.”
Qualified machines move through final inspection, packaging, and pre-shipment audit. Good factories run VFD quality control as a system rather than a single gate: incoming inspection for materials, in-process inspection during build, finished-product testing, and a pre-shipment check before the crate closes. Where a load bank is available, the unit is tested under real load by power range, which is the closest thing to proving performance rather than function.
Two things belong in every serious supplier’s answer at this stage, and neither is a wall decoration.
The first is the certificate file. A certificate on the wall proves nothing. What matters is a current document that names the legal entity that will invoice you. It should cover the model you are buying and be verifiable in the issuing body’s database. If the certificate names a different company than your invoice, stop and ask why.
The second is the test documentation that ships with the unit. A real drive comes with test records for that serial number. If a supplier cannot produce test data for a sample, the drive was either not properly tested or not built by the party you are talking to.
This is the same ground our full factory and certification audit checklist covers in detail, and we publish it knowing you will apply it to us.

Now the part that changes how you evaluate every supplier you meet. Here is each station, what a photo of it can tell you, and what it cannot.
| Station | What it does | What a photo proves | What it cannot prove | The question to ask |
|---|---|---|---|---|
| SMT line | Places and solders surface-mount parts | A line exists somewhere | That it is theirs, or that it builds your board | “Send a photo of the line holding a note with my name and today’s date” |
| AOI / inspection | Checks joint quality | Inspection is part of the process | That it inspects to IPC-A-610 Class 2 or 3 | “Which IPC-A-610 class do you build to, and who certifies your inspectors?” |
| Conformal coating | Protects against moisture, dust, and vibration | Coating is applied | That thickness is controlled | “How do you verify coating thickness?” |
| Torque-controlled assembly | Fasten the power devices to the heat sink | Parts are assembled | That torque is specified and controlled | “What torque spec do you use on the IGBT modules?” |
| Hi-pot | Verifies insulation and creepage | A test rig exists | That every unit is tested, or the pass rate | “Show me the hi-pot record for my serial numbers” |
| Functional test | Verifies circuits and functions | Units are powered and tested | That coverage is complete (it is near 98%) | “What is your functional-test coverage and pass rate?” |
| Aging / burn-in | Forces infant mortality out at high temperatures | A rack exists | That it is used, for how long, or with a log | “Send the aging log: serial, hours, temperature” |
| Final / load test | Verifies performance under load | Testing happens | That your model was load-tested | “Was my model load-tested, and at what load?” |
Read the table as a habit. A factory photo is evidence that a process exists. It is not evidence that the process will be applied to your order, with the right parameters, with a record you can check. The strongest single request in the whole list is the aging log, because it is the most expensive to fake and the most predictive of the unit you will actually receive.
Viktor, a plant engineer at a water utility, learned this on a shortlist. He had narrowed three suppliers to one on the strength of a polished photo set: gleaming SMT line, packed test benches, rows of finished drives. Before signing, he applied the table and asked two questions.
Which line would build his order, and what was the aging log for that model? The first answer named a line he had never seen a photo of. The second produced a log, but the hours did not match the model he had been quoted. The photos had come from a different site.
The supplier he eventually chose sent grittier images, a live video, and a log that matched his serial range exactly. “The pretty photo set cost that first supplier the contract,” he said. “The log won it for the second.”
Two more points remove the two most common false assumptions.
The outsourcing myth, stated plainly. A genuine VFD factory may outsource bare-board fabrication, and often does, because specialized PCB houses are more cost-effective and more technically advanced than an in-house line. This is normal industry practice, not a red flag. Judge a supplier on the stations it owns and controls, and above all on the ones that predict reliability: aging, hi-pot, and load test. If a supplier owns those, the origin of the bare board is a footnote.
The limit no photo can cross. No image proves that the factory you are shown is the factory that will build your order. Large manufacturers run multiple sites and lines, and a supplier may show you its best line while producing your units elsewhere. Close that gap directly: ask which line will build your order, and ask for the serial-ID range that line is currently producing. A supplier who can answer has a traceable process; one who cannot is showing you a brochure.
What does a VFD factory actually do?
It builds drives in two stages. It assembles and inspects the circuit board (or outsources the board and receives it tested), then builds the complete machine: assembly, hi-pot testing, functional test, 24 to 48-hour aging, final inspection, and packing.
How is a VFD made?
A variable frequency drive is made in two stages. A circuit board is assembled on an SMT line through paste printing, placement, reflow, and optical inspection. The board is then assembled into a complete unit with its power stage and cooling, hi-pot and functionally tested, aged at high temperature, inspected, and packed.
What is the difference between a VFD factory and a trading company?
A factory builds and tests the product. A trading company resells it, often without owning a line, an aging room, or test capability. Our China sourcing guide covers how to tell them apart, and the vetting checklist turns it into an audit.
Does a VFD manufacturer need its own SMT line?
No. Outsourcing bare-board fabrication, and often PCBA, is standard even for genuine manufacturers. Judge a factory on the stations it controls, especially aging, hi-pot, and load testing, rather than on whether it owns the board line.
What is an aging or burn-in test?
It runs a finished drive under power at elevated temperature, usually for 24 to 48 hours, to force early failures to appear in the factory. It is the most reliable single proof that the unit will survive its first weeks in your panel.
What is hi-pot testing on a VFD?
Hi-pot, or withstand-voltage testing, applies a high voltage to confirm that insulation and creepage between circuits hold. It is a safety and reliability gate, and every serious factory tests to it.
What should I look for on a VFD factory tour?
The stations that predict reliability: the aging room and its logs, the hi-pot rig, the functional and load test benches, and torque-controlled assembly. Ask for records, not rooms. A photo proves a process exists; a log proves it was used on your unit.
Can I audit a VFD factory remotely?
Yes, and it is now common. Ask for a live walkthrough of the production floor rather than a prepared video, time it to the burn-in racks and test benches, and request a handwritten note with your name and date in any photo you receive.
Here is how a VFD factory works, in one paragraph. The board is built on an SMT line, or outsourced to a specialist, then inspected to an IPC acceptance class. The complete machine is assembled with torque-controlled mounting, hi-pot tested, functionally tested, aged 24 to 48 hours at temperature, inspected, and packed with a certificate file that names the seller.
The stations that prove reliability are the test and aging stations, not the showroom ones. Photos show that a process exists; logs, serial-ID ranges, and certificate files show it was applied to your order.
That is the whole rubric, and it is the one we are happy to be measured against. Our factory runs these stations, and our engineers will walk you through them live, including the aging logs, against the same questions you would ask any supplier. Book a production-floor walkthrough or browse the drives we build and see the process behind them. If you need a customized or private-label build, our custom VFD manufacturing guide explains what changes on the line, and the full guide to choosing a manufacturer puts this tour in the wider selection framework.